
high-cod-battery-case-rinse-water-recycling-system--24-t/d-ro--edi-project, high-cod-battery-case-rinse-water-recycling-system--24-t/d-ro--edi-project, /case-studies
EN
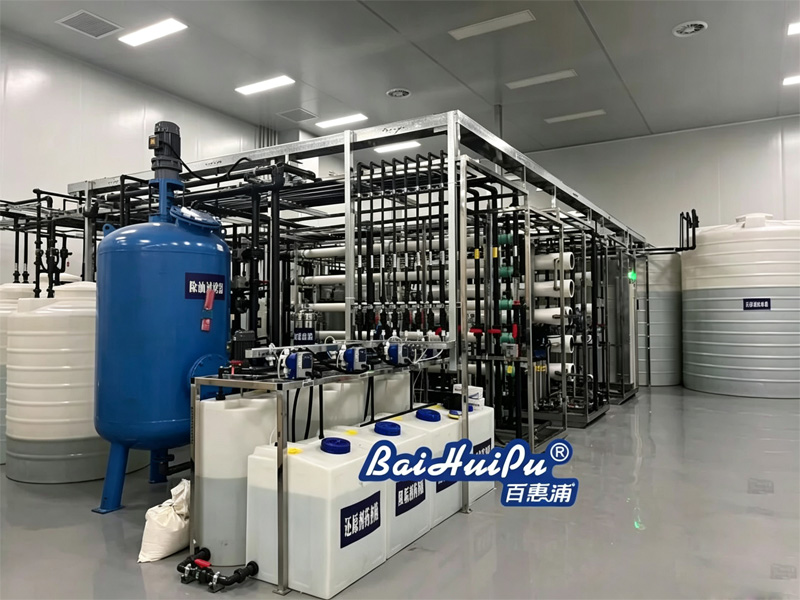
A membrane-based wastewater recycling solution featuring oil removal filtration, ultrafiltration (UF), pretreatment, three-pass reverse osmosis (RO), and EDI, designed for high-COD steel battery case rinsing wastewater without conventional physicochemical or biological treatment.
The customer is one of the world's leading manufacturers of high-performance green lithium batteries, possessing internationally advanced technologies and a fully integrated R&D platform covering battery materials, cells, BMS (Battery Management Systems), and complete battery systems.
Its products serve both consumer electronics and electric vehicle markets, providing comprehensive energy storage solutions for IoT applications and the global new energy industry.
Customer: Leading Lithium Battery Manufacturer
Application: Steel Battery Case Rinsing Wastewater Recycling
Treatment Capacity: 24 m³/day
Commissioning Year: 2024
Oil Removal Filter → Oil Removal Ultrafiltration (UF) → Pretreatment → Three-Pass Reverse Osmosis (RO) → Electrodeionization (EDI)
Product water resistivity: 10 MΩ·cm
The wastewater generated during steel battery case rinsing contains:
Traditional treatment methods generally rely on large biological or physicochemical treatment systems, which require extensive plant space, high operating costs, and significant maintenance.
For this project, Baihuipu developed an advanced membrane-based treatment solution capable of producing high-quality reclaimed water without conventional biological or chemical treatment processes.
To achieve both effective wastewater treatment and high-quality water reuse, Baihuipu designed the following integrated membrane treatment process.
The wastewater first passes through an oil removal filter to efficiently separate free oil and the majority of floating grease, reducing the load on downstream membrane equipment.
Following primary oil separation, the wastewater enters an ultrafiltration system.
The UF membranes further remove emulsified oil, suspended solids, and fine particulate matter, providing excellent pretreatment for the reverse osmosis system.
Additional pretreatment using multimedia sand filtration and activated carbon filtration removes residual suspended particles, organic impurities, and trace contaminants, maximizing membrane protection and extending equipment service life.
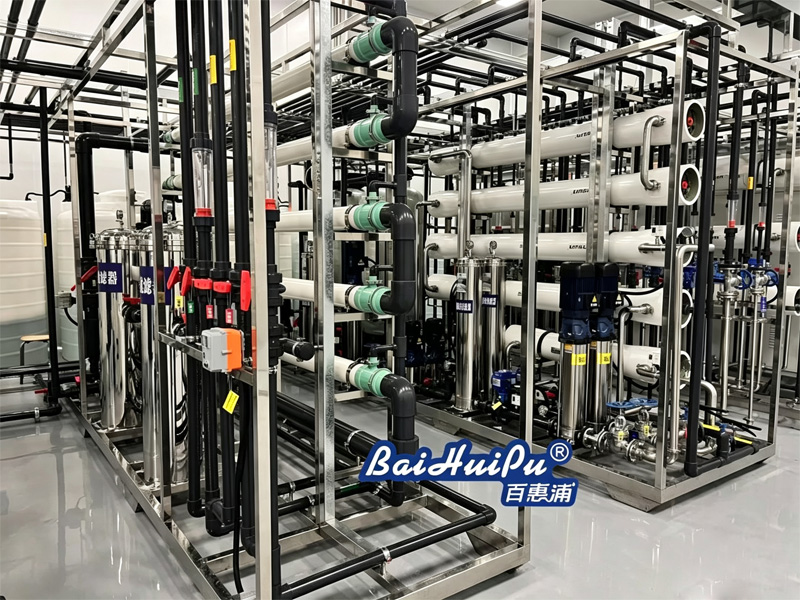
The core of the system consists of a three-pass reverse osmosis (RO) system combined with Electrodeionization (EDI).
The RO membranes effectively remove:
The multi-stage RO configuration significantly improves desalination efficiency and overall water quality.
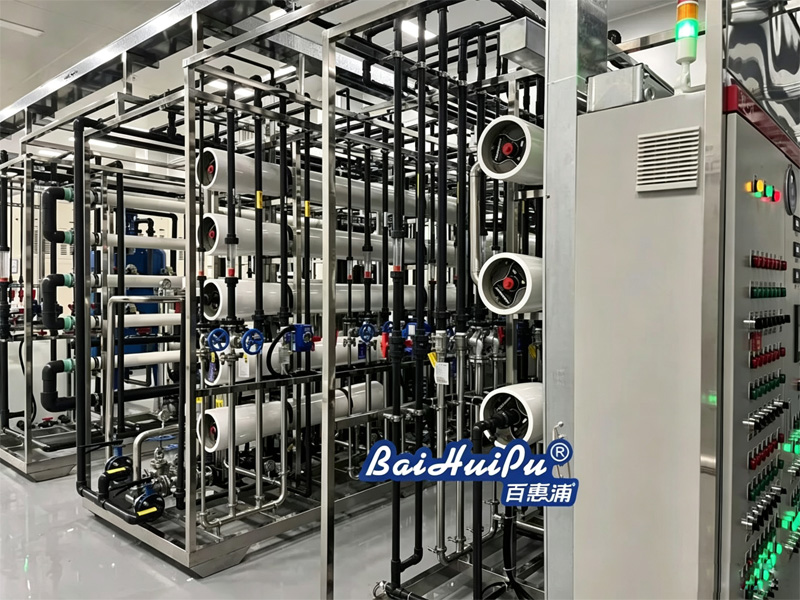
Following RO treatment, water enters the EDI unit.
Using a combination of high-voltage electric fields, ion exchange resins, and ion-selective membranes, EDI continuously removes residual ionic contaminants without chemical regeneration.
The system consistently produces ultrapure water with a product water resistivity of 10 MΩ·cm, fully satisfying the customer's process water requirements.
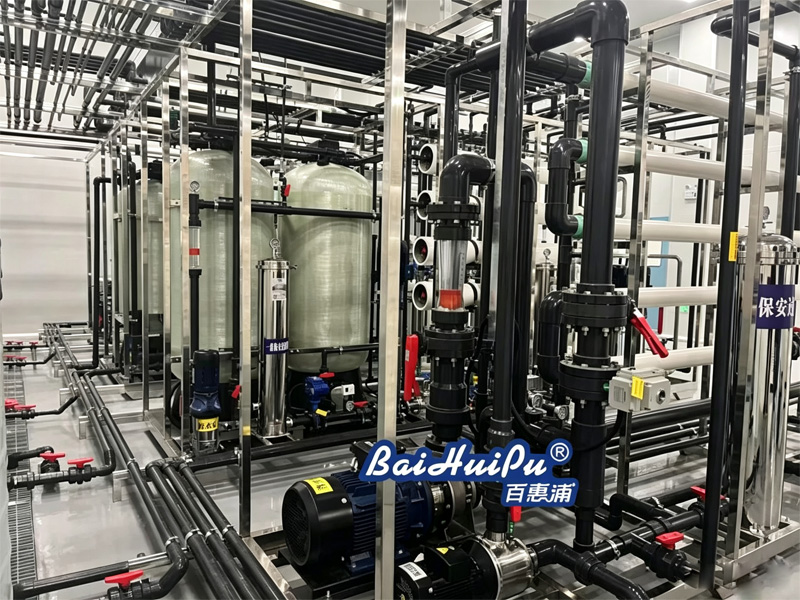
The integrated membrane system consistently produces reclaimed water with a resistivity of 10 MΩ·cm, providing reliable process water for battery manufacturing.
Unlike conventional wastewater treatment systems, this solution eliminates the need for:
This significantly simplifies plant operation while reducing maintenance requirements.
The optimized membrane process minimizes chemical consumption, reduces sludge generation, and lowers overall operating and maintenance costs throughout the system lifecycle.
The complete treatment system operates with excellent long-term stability, delivering consistent water quality while requiring minimal operator intervention.
The modular membrane-based design requires substantially less installation space than conventional wastewater treatment plants, making it ideal for battery manufacturing facilities with limited available floor area.
This successful project demonstrates Baihuipu's expertise in applying advanced membrane technologies to the treatment and recycling of high-COD industrial wastewater generated by lithium battery manufacturing.
By combining oil removal filtration, ultrafiltration, three-pass reverse osmosis, and EDI, the system achieves stable production of high-quality reclaimed water without relying on traditional biological or physicochemical treatment processes.
Since commissioning in 2024, the system has operated reliably, consistently producing reclaimed water that meets the customer's production requirements while significantly reducing freshwater consumption and supporting sustainable manufacturing.
The project provides a valuable reference for similar high-COD battery manufacturing wastewater recycling applications and further strengthens Baihuipu's position as a provider of advanced industrial water treatment and water reuse solutions for the global lithium battery industry.

 EN