bhp-mother-liquid-drying-system--industrial-wastewater-residue-drying--solidification-equipment, bhp-mother-liquid-drying-system--industrial-wastewater-residue-drying--solidification-equipment, /mother-liquor-drying-unit
EN
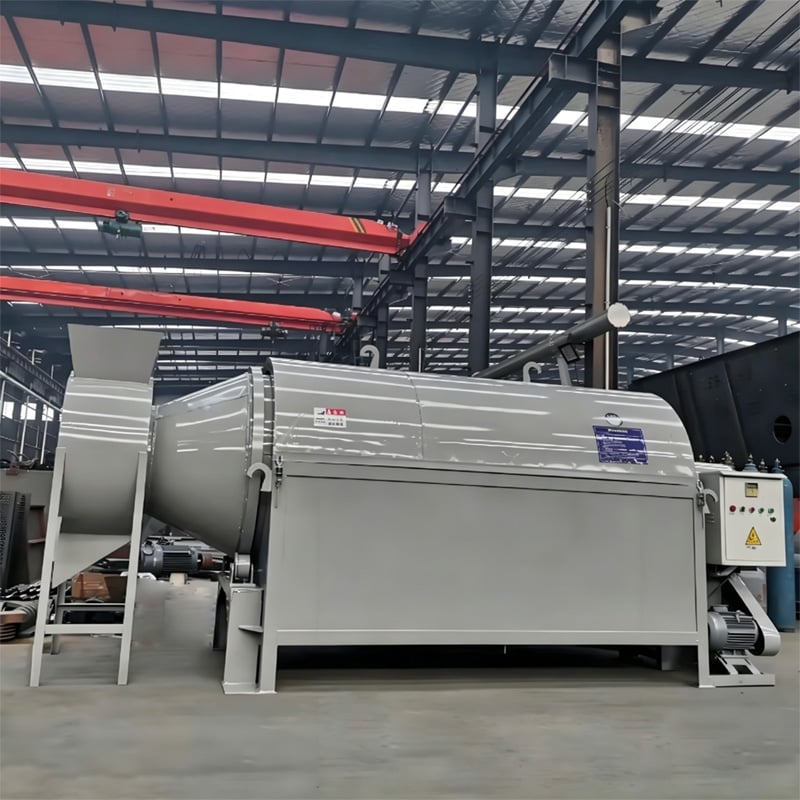
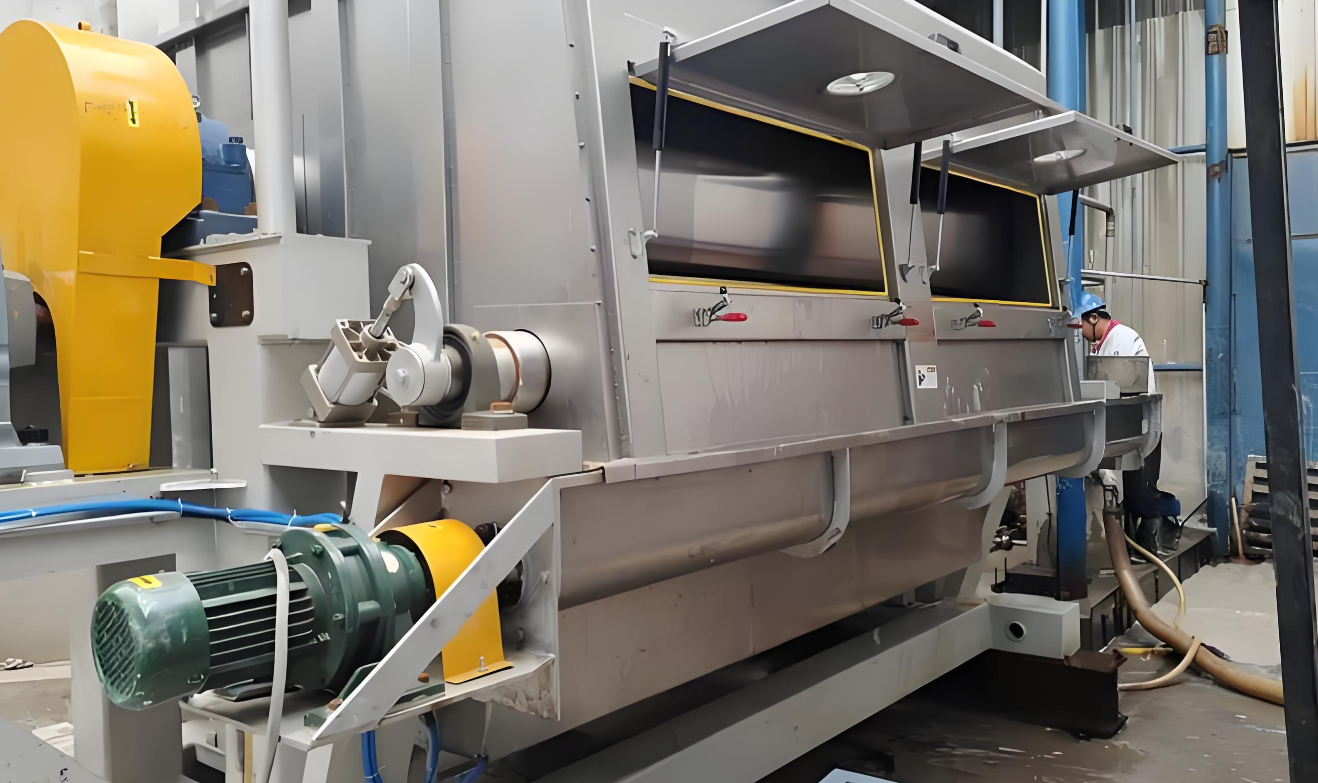
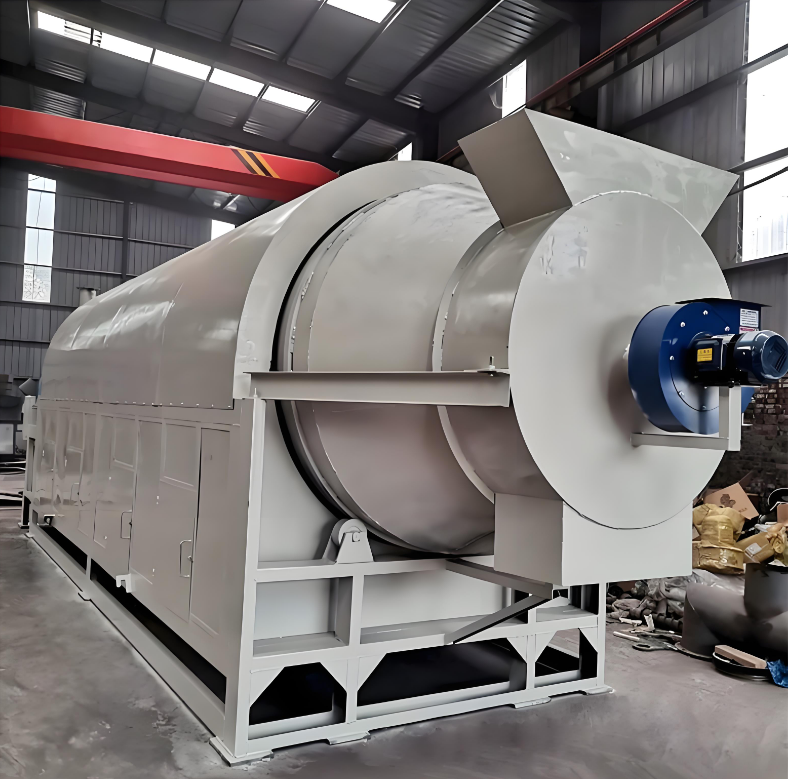
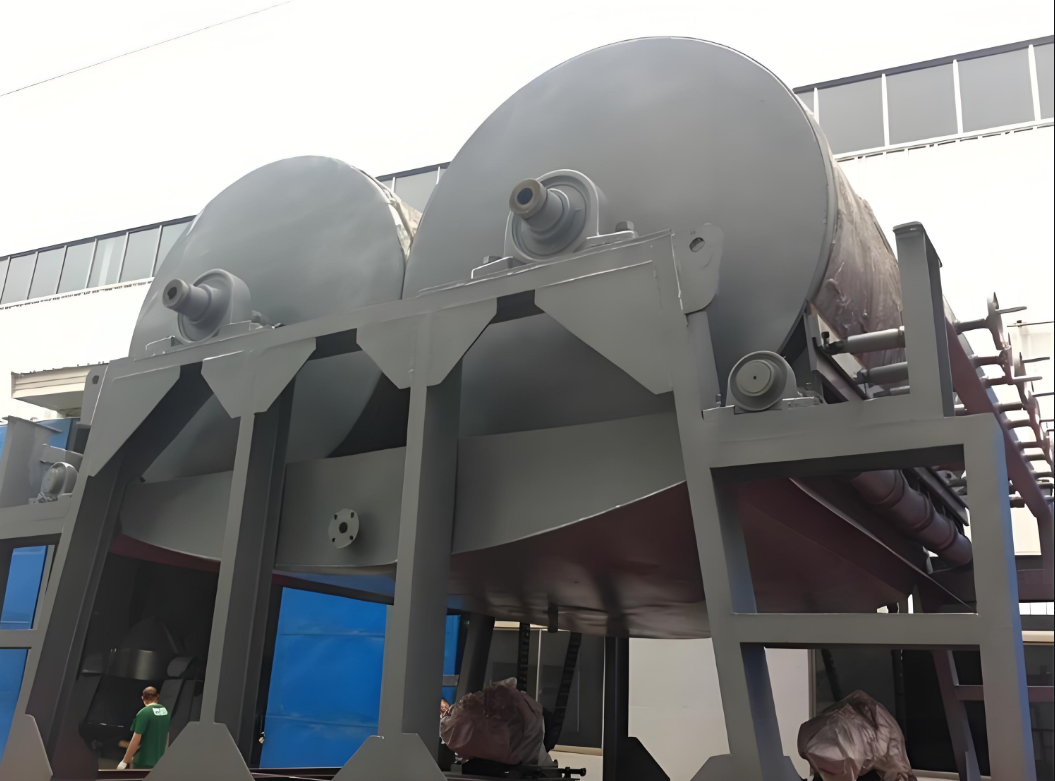
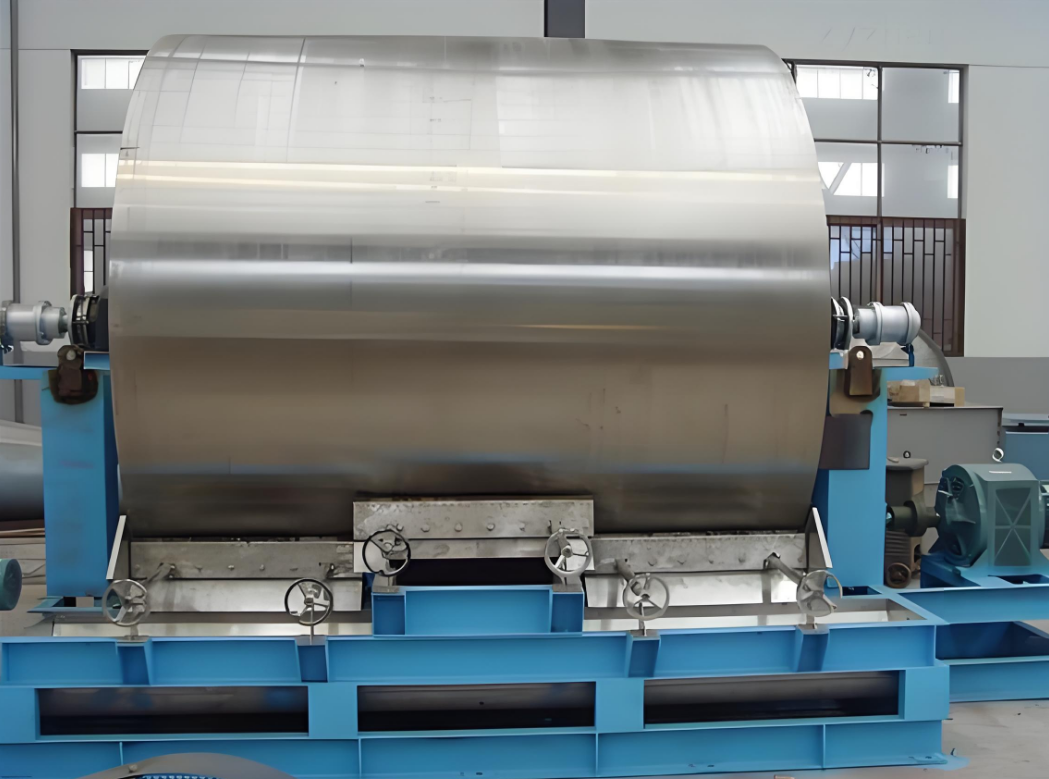
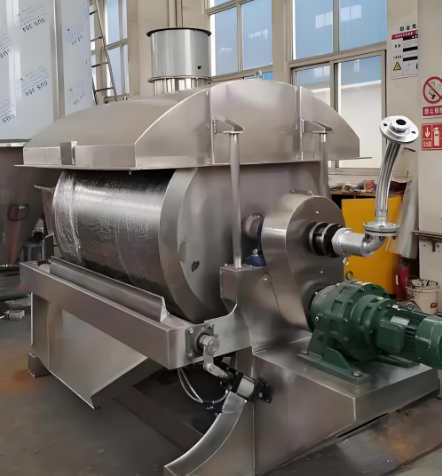
BHP mother liquid drying system, 0.5-50T/H, low-temperature (45-85°C) solidification, ≥95% volume reduction, for ZLD final-stage residue management.
The BHP Mother Liquid Drying System is industrial wastewater residue drying & solidification equipment engineered specifically for high-salinity mother liquor treatment. This final-stage system addresses the most persistent compliance gap in zero liquid discharge (ZLD) technology: the concentrated residual mother liquor that conventional evaporation and salt-separation processes cannot eliminate. By applying low-temperature circulating hot-air technology, the BHP Mother Liquid Drying System converts liquid waste into dry solid salt residue, enabling complete zero liquid discharge at the facility level.
In ZLD projects, primary evaporation and crystallization units process the bulk of high-salinity wastewater — but they leave behind saturated, concentrated mother liquor. This residual stream carries high viscosity, complex mixed-salt composition, and elevated organic content preventing further crystallization. Without dedicated industrial wastewater residue drying & solidification equipment at the final stage, facilities face a secondary waste management problem: the mother liquor cannot be discharged, reused, or sold, leaving costly landfill disposal as the only option.
| Parameter | Specification |
|---|---|
| Brand | BHP |
| Model Series | BHP-MLDS Series |
| Capacity Range | Custom from 0.5–50 T/H |
| Core Technology | Low-temperature hot air drying + residual liquid solidification treatment |
| Suitable Feed | Evaporation mother liquor, concentrated brine, high-salinity residual liquid, saturated waste liquid |
| Drying Temperature | 45℃–85℃ (low-temperature range to prevent material decomposition) |
| Volume Reduction | ≥95% reduction in residue volume |
| Final Product | Dry solid salt residue with no free liquid |
| Control System | Fully automatic PLC control for continuous, unattended operation |
| Material of Construction | Corrosion-resistant 316L stainless steel or titanium alloy |
| Operating Feature | Low energy consumption, anti-caking design, uniform drying |
| Certification | ISO9001, ISO14001, CE |
Environmental compliance specialists evaluating zero liquid discharge technology consistently encounter the same limitation: after investing in MVR evaporators and salt-separation systems, a facility still generates a mother liquor concentrate containing residual organics and trace metals that cannot be discharged, reused, or sold. This is an inherent limitation of crystallization chemistry — not an equipment failure — and it creates a measurable compliance gap under zero-discharge environmental permits.
The final mother liquor fraction concentrates all impurities excluded from the primary crystal product: a high-viscosity, near-saturated mixture of salts and organics that resists further crystallization. Resolving this gap requires industrial wastewater residue drying & solidification equipment capable of handling this chemically complex stream. The BHP Mother Liquid Drying System is engineered specifically for this application — converting the concentrated residual stream into dry solid residue and eliminating the final source of liquid discharge.
The choice between low-temperature drying and atmospheric evaporation for this final stage depends critically on feed composition. When residual mother liquor contains heat-sensitive organic compounds — common in pharmaceutical, battery material, and fine chemical production — low-temperature drying at 45–85°C prevents decomposition of organic components and avoids harmful gas generation.
The BHP Mother Liquid Drying System eliminates the remaining liquid discharge source, enabling facilities to achieve full ZLD permit compliance. By converting concentrated organic-salt liquor into stable dry solid, this industrial wastewater residue drying & solidification equipment closes the final compliance gap in the ZLD treatment chain.
Complete solidification achieves more than 95% volume reduction in residue, greatly reducing solid-waste storage and disposal costs. For facilities under ZLD mandates — increasingly required across water-scarce regions and industries handling hazardous effluents — this volume reduction translates to lower logistics costs and simpler regulatory documentation.
The low-temperature drying design prevents heat-related decomposition of salt components and avoids generation of harmful gases. Operating temperature is maintained below decomposition thresholds for common salt species — particularly important for battery industry mother liquor containing lithium salts and pharmaceutical wastewater with trace active ingredients.
High-grade corrosion-resistant materials — 316L stainless steel and titanium alloy — provide reliable long-term performance when treating highly corrosive saturated mother liquor. Based on industrial wastewater treatment projects involving concentrated brine streams, material selection is one of the most controllable factors determining long-term equipment reliability.
Full automatic PLC controls manage feeding, constant-temperature drying, solid-residue discharge, and fault alarms, reducing daily operating requirements. The BHP Mother Liquid Drying System supports continuous unattended operation and optional remote cloud monitoring.
The BHP Mother Liquid Drying System integrates with BHP MVR evaporators, single-effect and multiple-effect evaporators, and salt-separation systems to create a complete closed-loop solution for industrial wastewater residue drying & solidification.
The BHP Mother Liquid Drying System serves final-stage industrial wastewater residue drying & solidification needs across six primary sectors:
From experience with BHP Mother Liquid Drying System installations, nozzle fouling in early commissioning typically traces to feed concentration instability. When upstream MVR evaporator outlet concentration varies beyond design range, atomization becomes unstable and semi-dry particles adhere to chamber walls. The BHP-MLDS incorporates a concentration equalization buffer at the feed inlet to stabilize feed quality and reduce nozzle fouling frequency.
Facilities implementing industrial wastewater residue drying & solidification equipment should plan solid residue management from project inception. Engaging local solid waste classification authorities early clarifies whether dry residue qualifies as general industrial solid waste or hazardous waste, determining disposal logistics and cost structure over the operational life.
The BHP Mother Liquid Drying System is compatible with BHP MVR evaporators, salt-separation systems, RO water-reuse systems, and pretreatment filtration equipment, creating a complete closed-loop solution for high-salinity wastewater treatment and zero liquid discharge.
The BHP-MLDS Series — industrial wastewater residue drying & solidification equipment — is certified to ISO9001, ISO14001, and CE marking requirements, supporting project approval documentation for European and international procurement processes.
BHP mother liquid drying system, 0.5-50T/H, low-temperature (45-85°C) solidification, ≥95% volume reduction, for ZLD final-stage residue management.

 EN