
chicago-usa-lithium-battery-integrated-water-treatment--ultrapure-water-slurry-recovery--wastewater-reuse, chicago-usa-lithium-battery-integrated-water-treatment--ultrapure-water-slurry-recovery--wastewater-reuse, /case-studies
EN
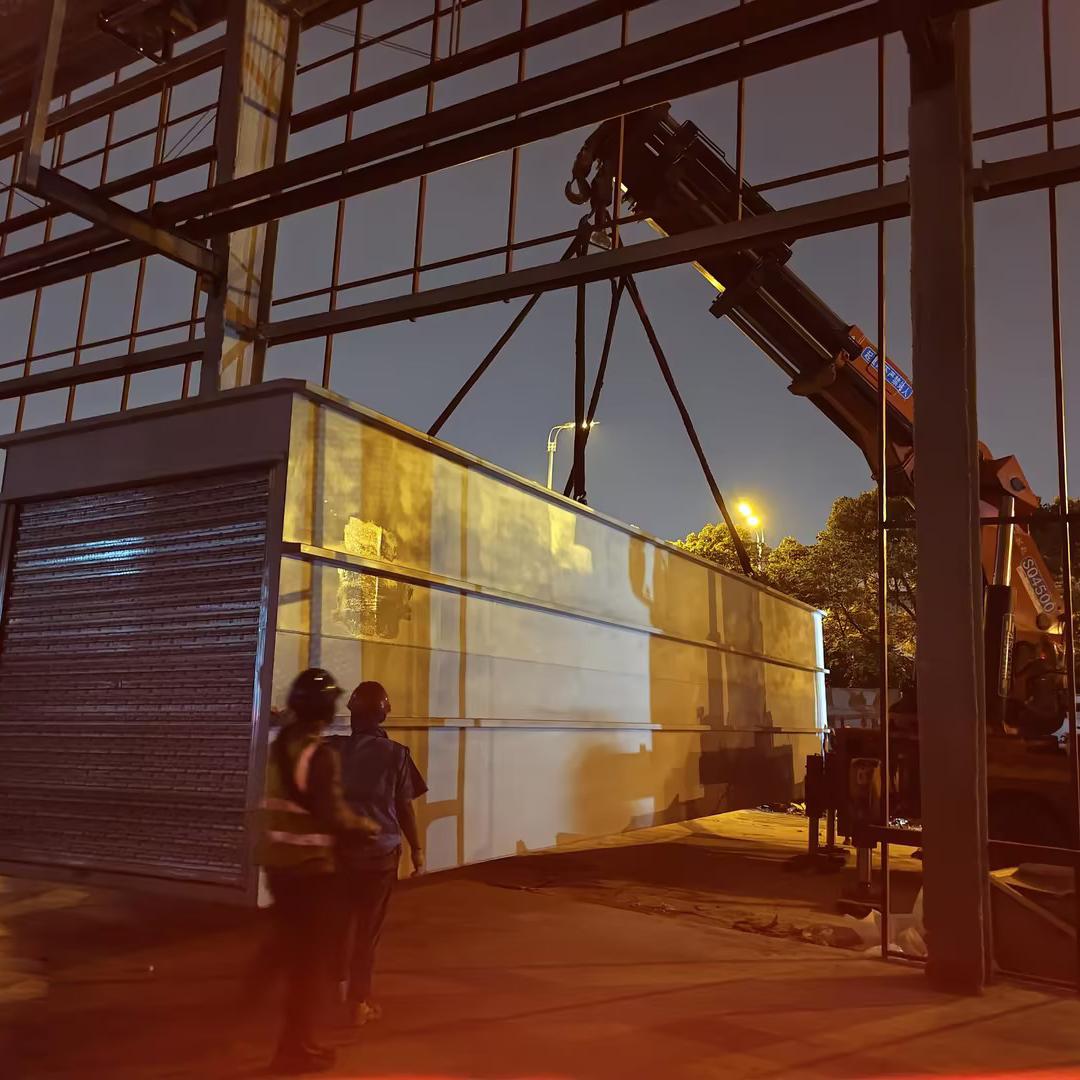
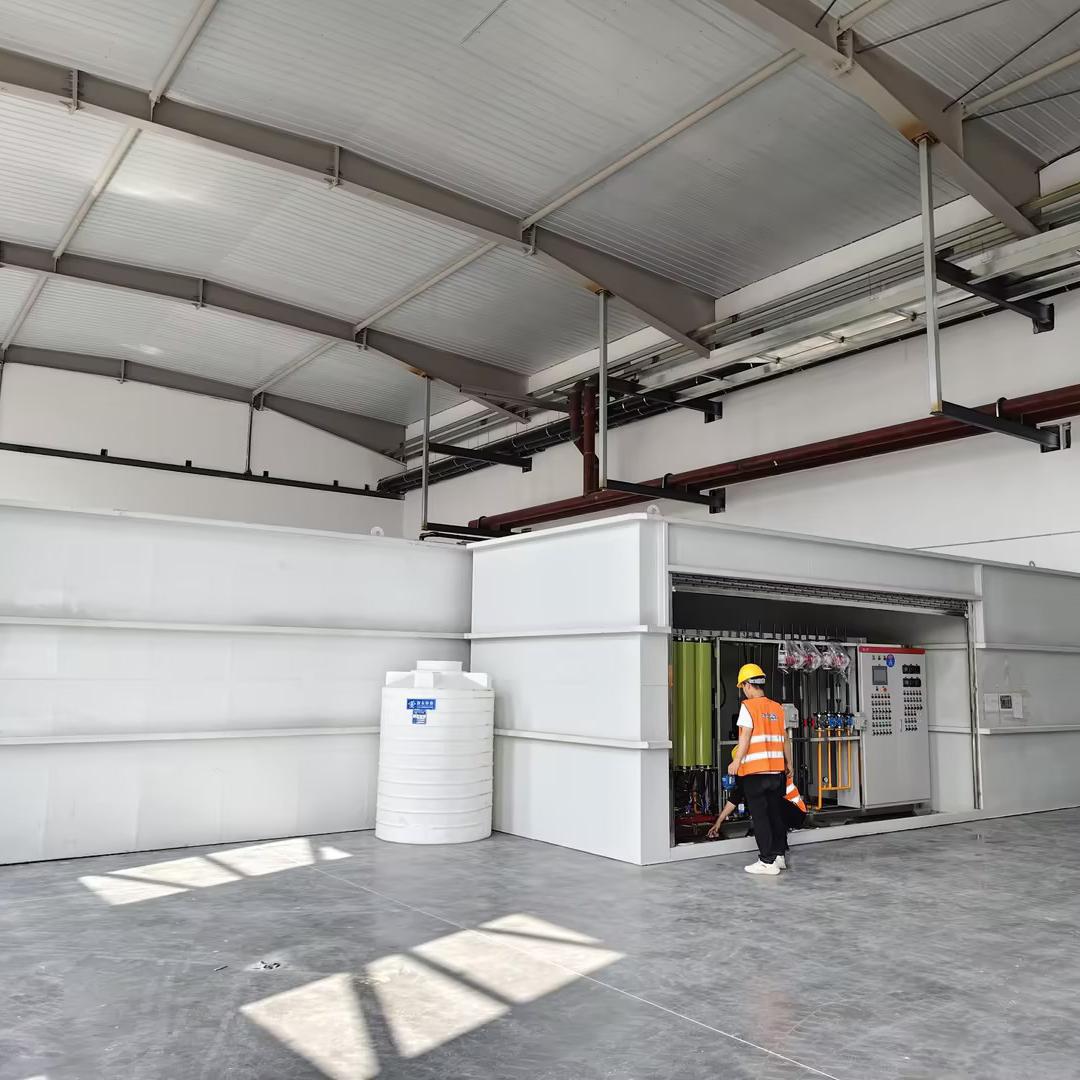
Designed for North American lithium battery manufacturing facilities, this integrated system combines a 10 T/H ultrapure water plant, 15 T/D battery slurry recovery unit, and 40 T/D wastewater recycling system. It recovers valuable NMP solvent and electrode slurry while treating industrial wastewater for compliant reuse in accordance with U.S. environmental regulations.
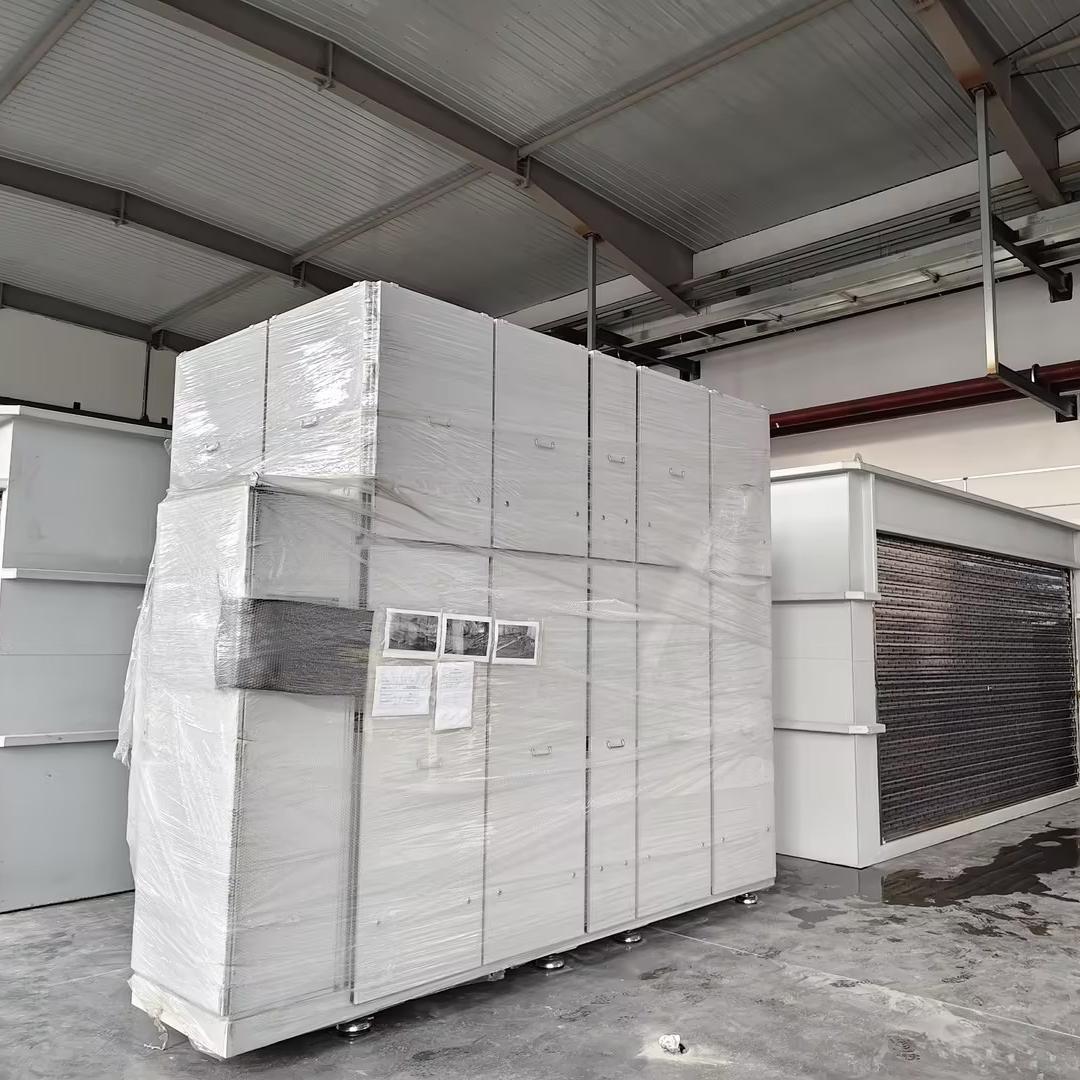
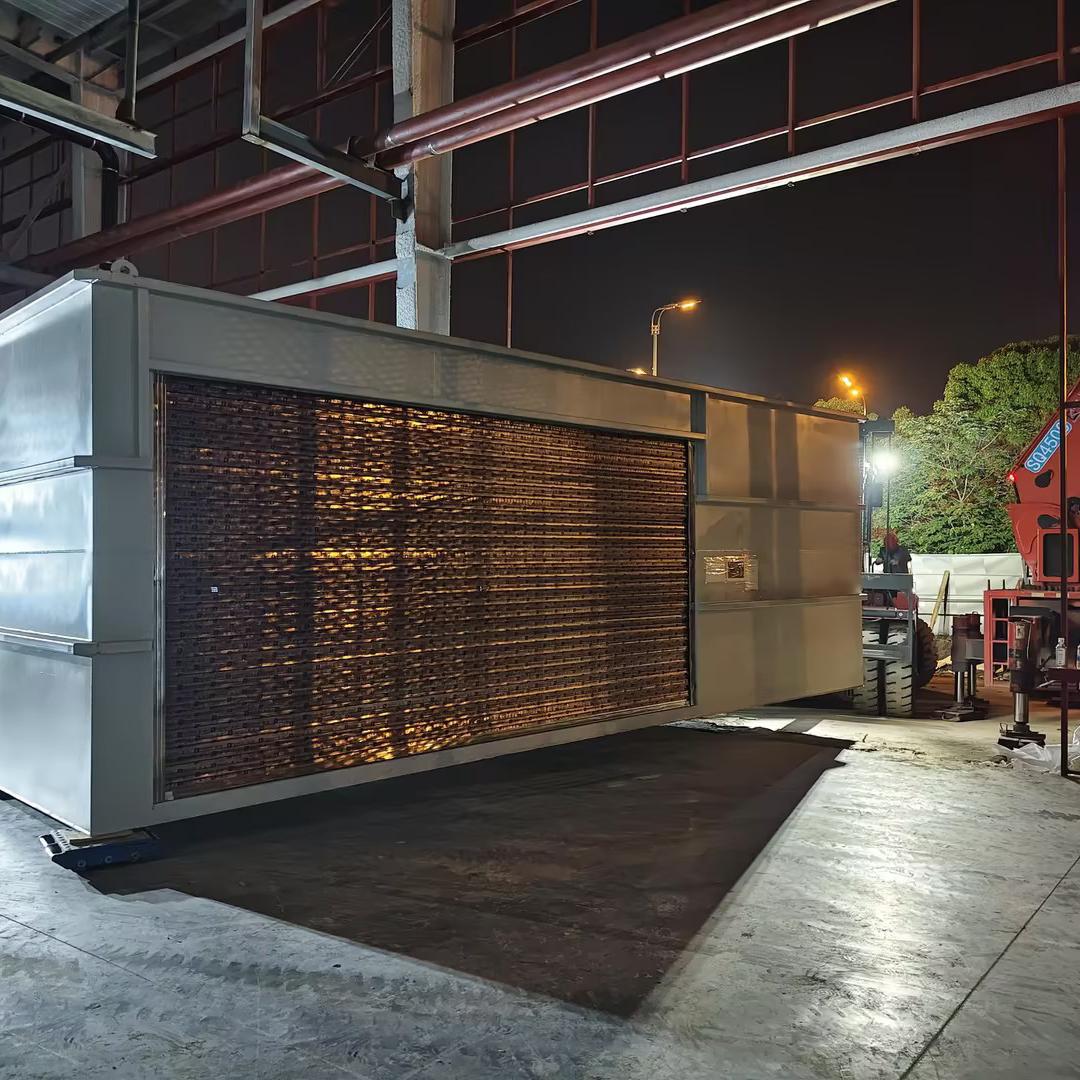
This integrated water treatment project was installed at a new energy battery manufacturing facility in Chicago, USA, with an overall treatment capacity of 41 m³/day. The complete solution consists of three interconnected process modules:
1. Ultrapure Water Production
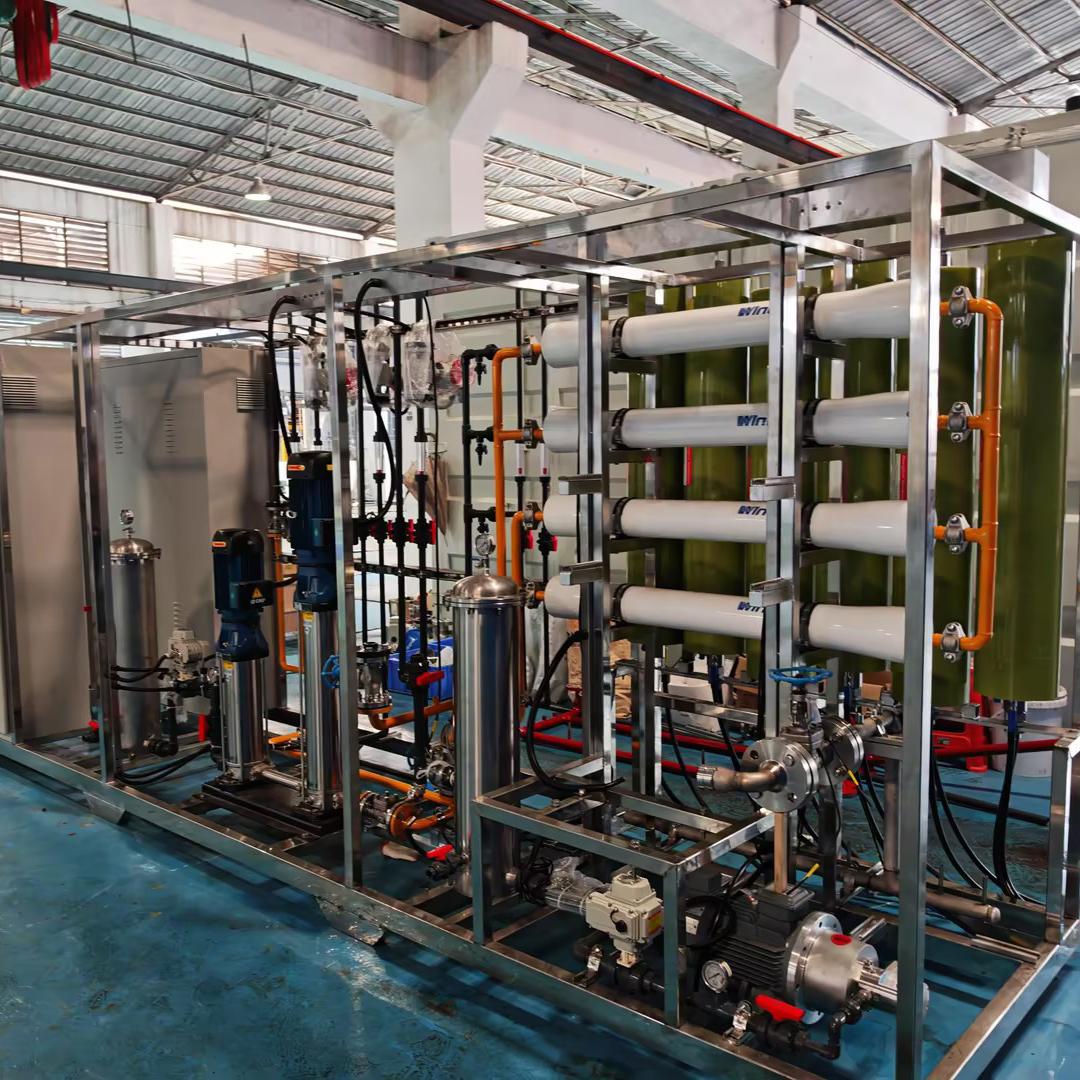
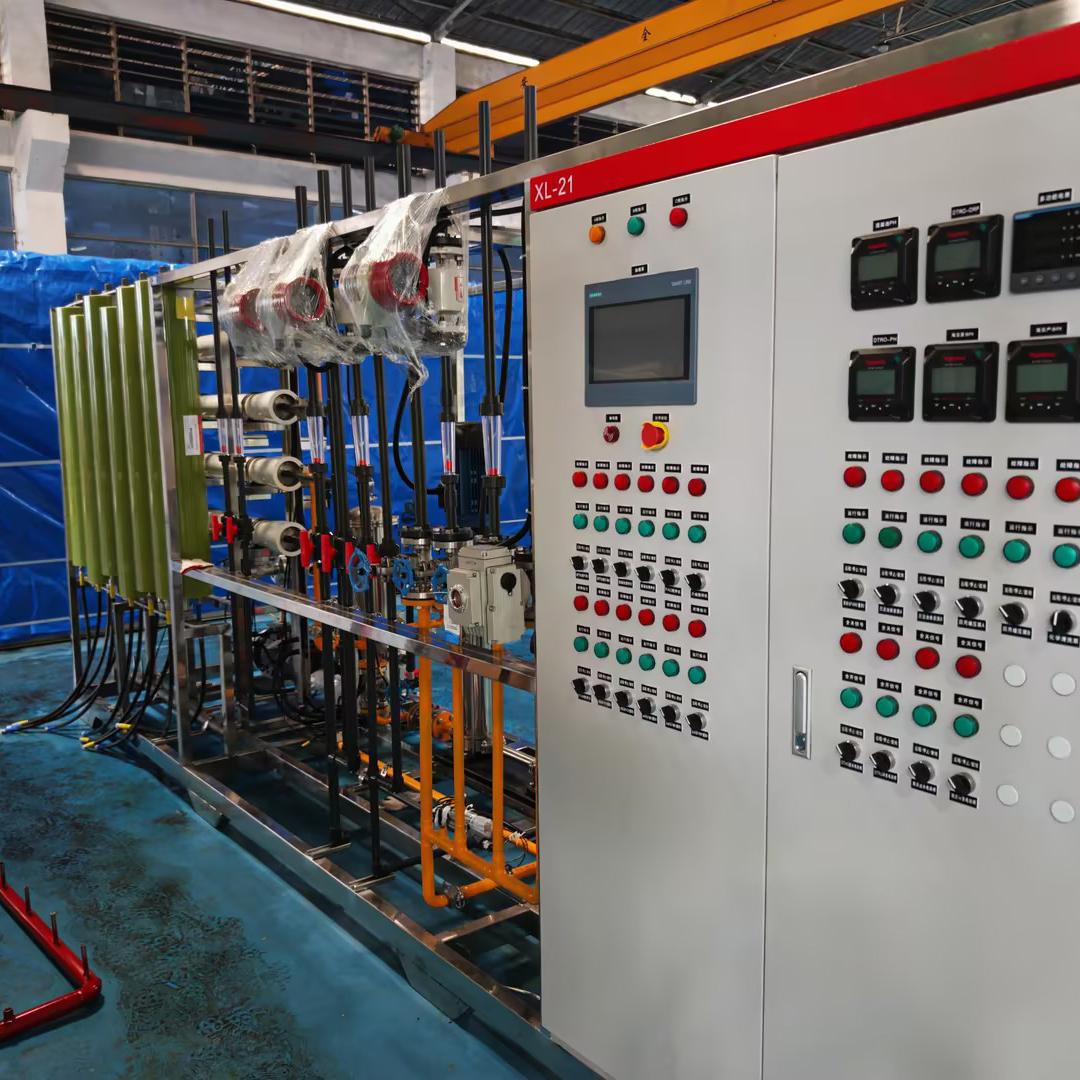
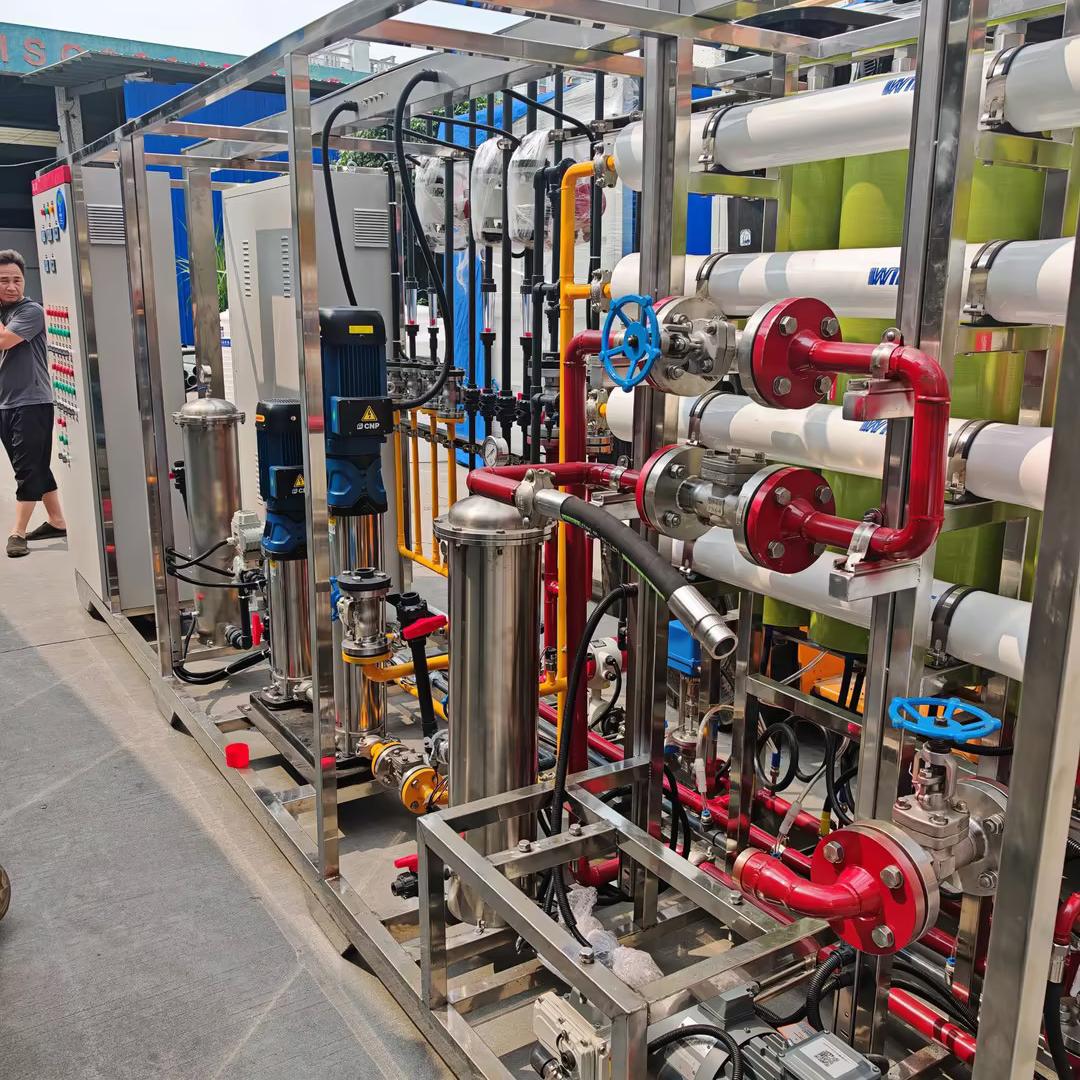
Raw Water → Pretreatment → Two-Pass Reverse Osmosis (RO) → Electrodeionization (EDI) → Mixed-Bed Polishing
The system continuously produces 10 tons/hour of ultrapure water for battery electrode coating, equipment cleaning, and other high-purity production processes.
2. Battery Slurry Recovery
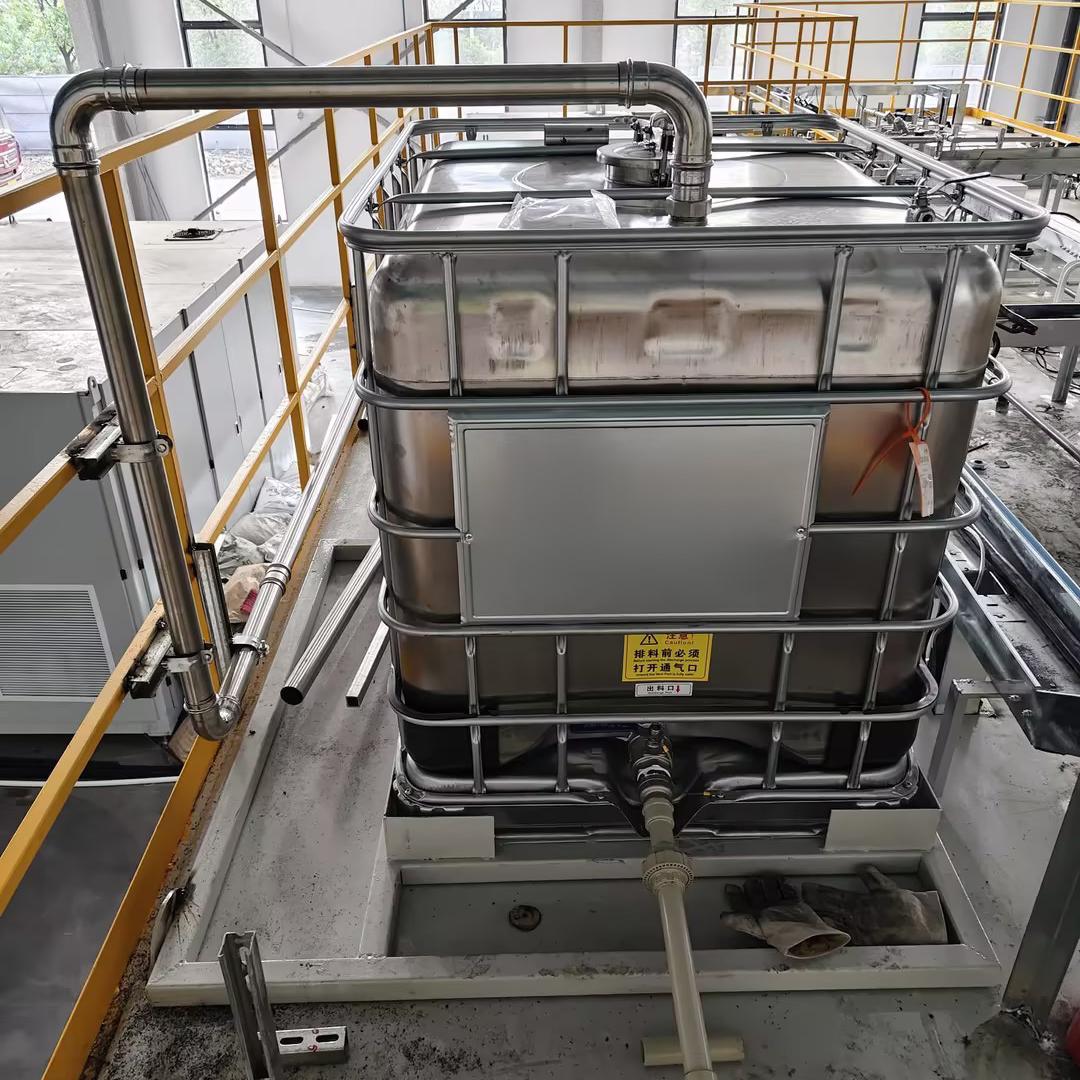
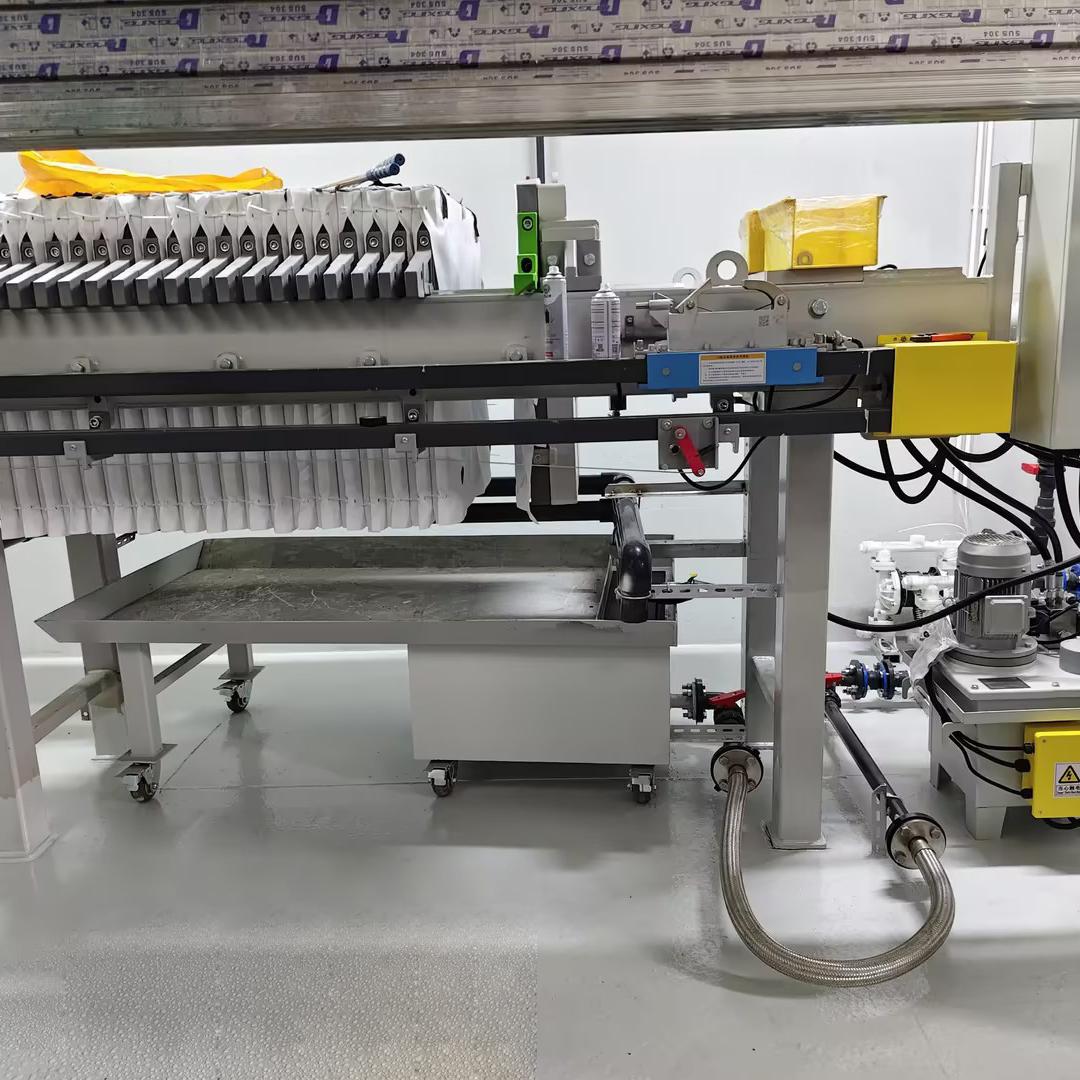
Battery slurry wastewater is fed into the integrated recovery unit, where valuable NMP (N-Methyl-2-pyrrolidone) solvent and solid electrode materials are separated and recovered for reuse, significantly reducing raw material consumption.
3. Wastewater Treatment & Recycling
Recovered slurry filtrate combined with other production wastewater follows the treatment process below:
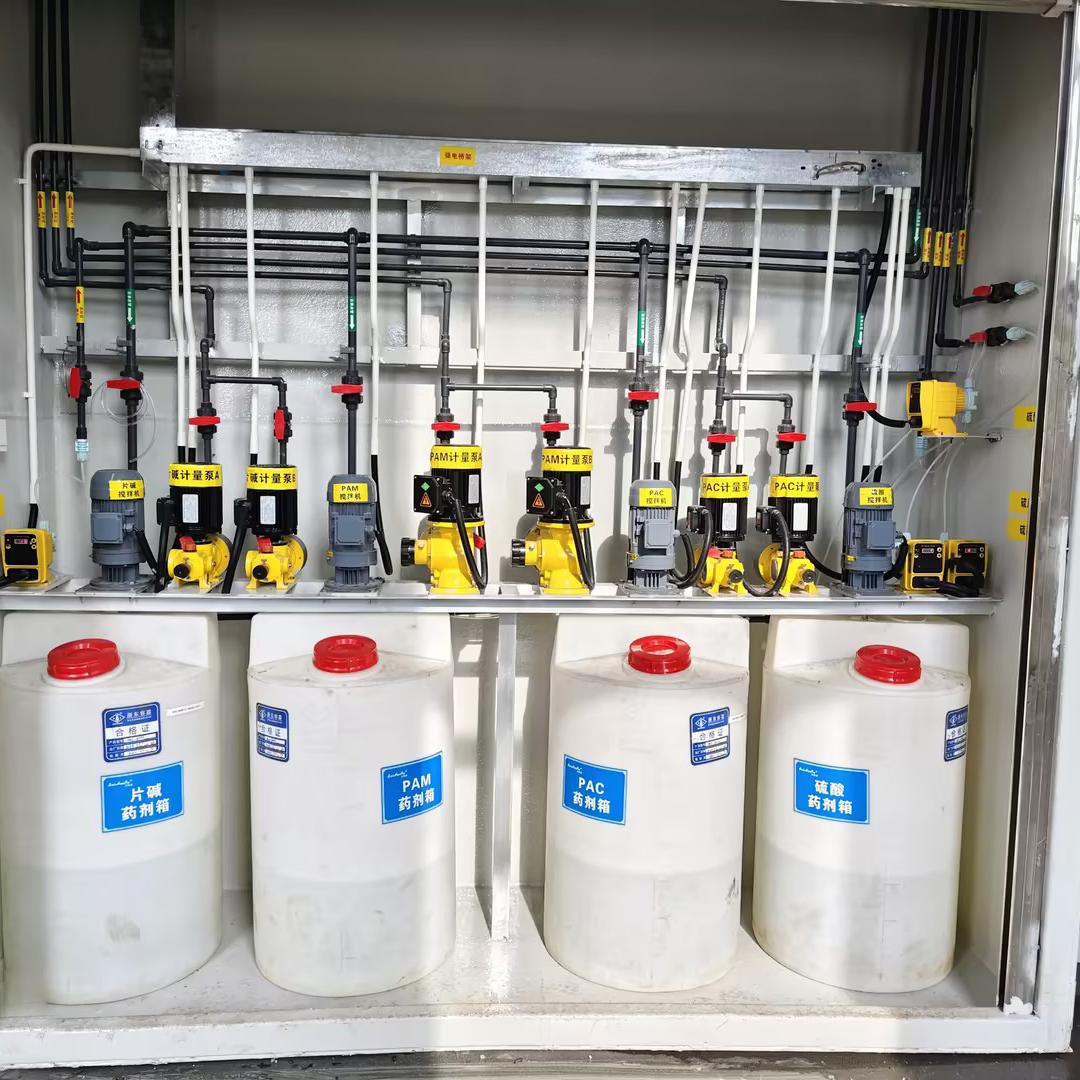
pH Adjustment Tank → Acidification & Coagulation Sedimentation → Fenton Advanced Oxidation → Hydrolytic Acidification + A/O-MBR Biological Treatment → Activated Carbon Filtration + Sand Filtration → Reclaimed Water Tank
The system treats 40 tons/day of industrial wastewater and supplies reclaimed water back to the production facility.
System Features
 |
 |
 |
 |
This integrated water treatment solution is specifically designed for lithium-ion battery, EV battery, energy storage battery and new energy battery manufacturers throughout the United States and North America.
It serves the complete battery production process, including:
Battery manufacturing generally faces two major challenges:
The integrated solution simultaneously delivers:
making it ideal for:
The system fully complies with the stringent environmental and hazardous waste management requirements of North America.
 |
 |
 |
 |
As the North American lithium battery and energy storage industry continues to expand rapidly, battery manufacturers in the Chicago area require reliable solutions for both high-purity process water and industrial wastewater resource recovery. Battery electrode coating, slurry preparation and precision cleaning processes demand a continuous supply of ultrapure water, while wastewater generated during production contains valuable NMP solvent and electrode materials.
Traditional standalone treatment systems are typically fragmented, occupy large floor space and offer limited recovery efficiency. Valuable NMP solvent and battery slurry are often discarded together with wastewater, increasing raw material costs while creating significant environmental compliance challenges due to the high organic load and solvent content.
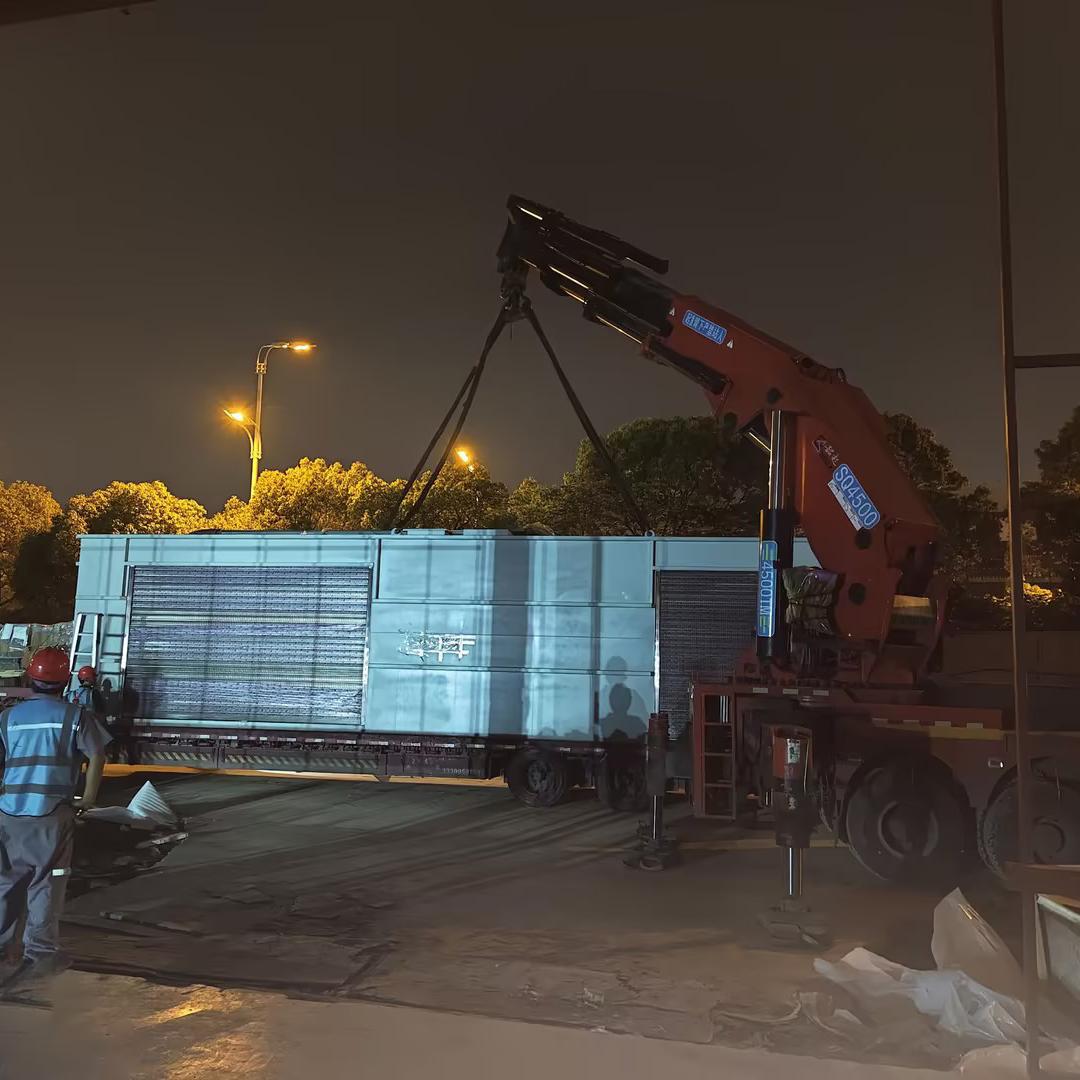
To address these issues, Baihuipu engineered a fully integrated water treatment solution that combines ultrapure water production, slurry recovery and wastewater recycling into one automated system with an overall treatment capacity of 41 m³/day. The integrated design is particularly suitable for overseas battery manufacturing facilities requiring high automation and minimal manual operation.
Incoming raw water first enters the ultrapure water system, where suspended solids and residual chlorine are removed during pretreatment. Water is then purified through a two-pass RO system, followed by EDI and mixed-bed polishing to continuously produce 10 T/H of high-quality ultrapure water for battery electrode coating and precision cleaning applications, ensuring stable manufacturing quality.
Battery slurry wastewater is separately processed through the 15 T/D slurry recovery unit, where membrane separation technology efficiently recovers valuable NMP solvent and solid electrode materials. These recovered materials can be directly returned to the slurry preparation process, significantly reducing raw material procurement costs.
The remaining wastewater is combined with other production wastewater and enters the 40 T/D wastewater treatment and recycling system. Following pH adjustment and coagulation sedimentation to remove suspended solids and colloidal contaminants, the wastewater undergoes Fenton advanced oxidation, effectively breaking down refractory organic compounds and reducing COD levels. Subsequent Hydrolytic Acidification + A/O-MBR biological treatment further degrades residual organic pollutants. Final polishing through activated carbon and sand filtration produces reclaimed water suitable for equipment cooling, floor cleaning and other industrial reuse applications, substantially reducing freshwater consumption.
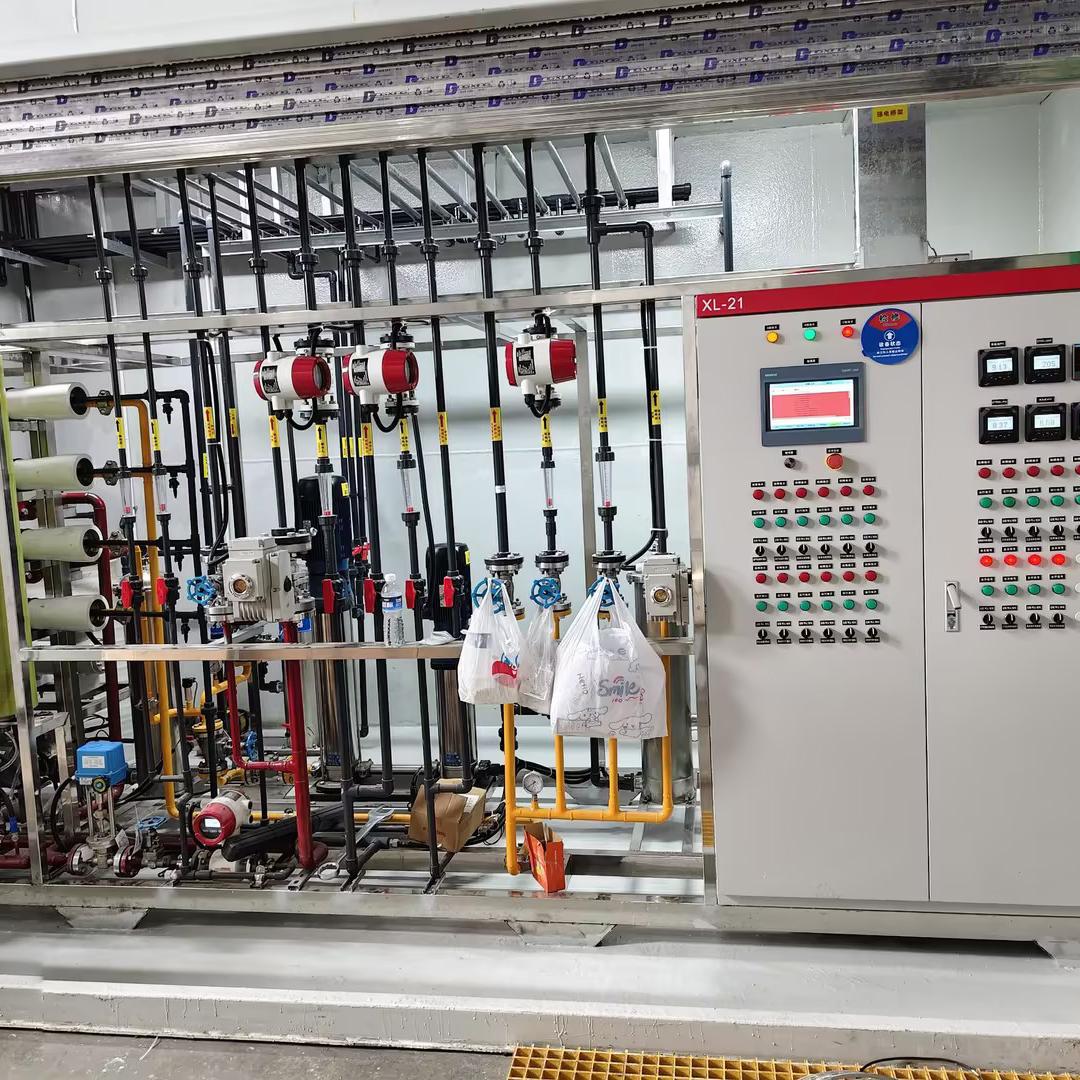
The entire system operates automatically under a PLC-based intelligent control platform with remote monitoring capabilities. Designed to meet North American electrical specifications and environmental compliance requirements, the project provides reliable ultrapure water production, recovers valuable battery materials, and enables efficient wastewater recycling while helping manufacturers reduce operating costs and achieve sustainable production.
This project represents a benchmark integrated water treatment solution for overseas lithium battery and energy storage manufacturing facilities.
 |
 |
 |
 |

 EN