
new-energy-battery-wastewater-treatment-system--anhui-project-case, new-energy-battery-wastewater-treatment-system--anhui-project-case, /case-studies
EN
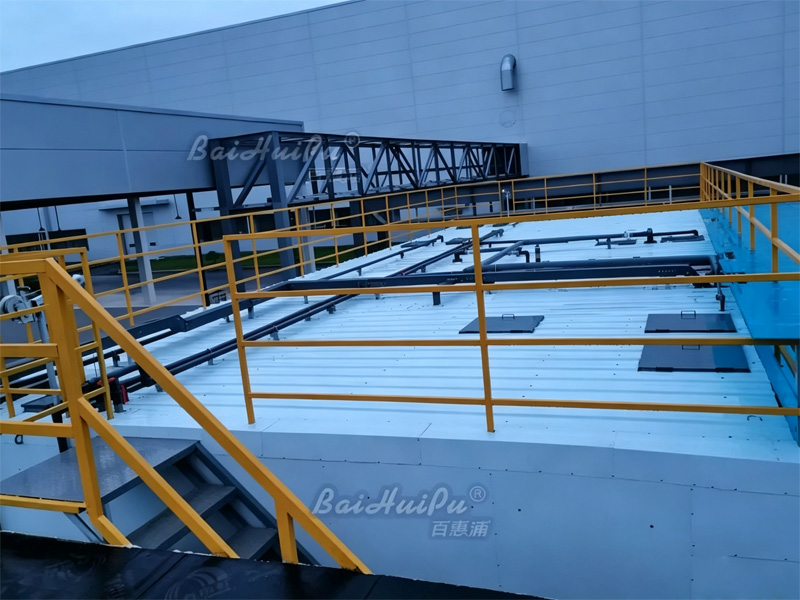
A customized lithium battery wastewater treatment solution integrating Fenton advanced oxidation, multi-stage biological treatment, and MBR membrane technology to efficiently remove heavy metals, refractory organics, COD, ammonia nitrogen, and total nitrogen, ensuring stable compliance with China's battery industry discharge standards.
The customer is a leading new energy battery manufacturer in Anhui Province, China, specializing in advanced lithium-ion battery manufacturing and intelligent battery production technologies.
The company has established a strategic partnership with 24M Technologies to develop next-generation semi-solid-state and solid-state battery technologies, creating an advanced manufacturing platform for high-performance battery products.
Physicochemical Pretreatment (Fenton Coagulation & Sedimentation) → Anaerobic (A) → Anoxic (A) → Aerobic (O) → Anaerobic (A) → Aerobic (O) → MBR Membrane Bioreactor → Compliant Discharge
Designed to comply with the Pollutant Discharge Standard for the Battery Industry.
Following a comprehensive site survey and wastewater quality analysis, Baihuipu's engineering team designed a fully integrated wastewater treatment solution consisting of four major treatment stages.
Wastewater first undergoes pH adjustment to convert dissolved heavy metal ions into insoluble precipitates. Coagulation, flocculation, sedimentation, and precision filtration are then applied to remove suspended solids together with a significant portion of high-molecular-weight organic compounds.
The pretreated wastewater enters the Fenton Advanced Oxidation Process (AOP).
Hydroxyl radicals generated during the reaction effectively break down refractory organic compounds that are difficult to biodegrade, significantly improving wastewater biodegradability and reducing the treatment load on downstream biological processes.
The wastewater is subsequently treated through a series of:
Specialized microbial communities metabolize the remaining organic pollutants while simultaneously removing ammonia nitrogen (NH₃-N) and total nitrogen (TN), achieving highly efficient biological purification.
The final biological effluent is treated using Membrane Bioreactor (MBR) technology.
The membrane system efficiently separates activated sludge and trace suspended contaminants, producing a consistently high-quality effluent that fully complies with national discharge standards.
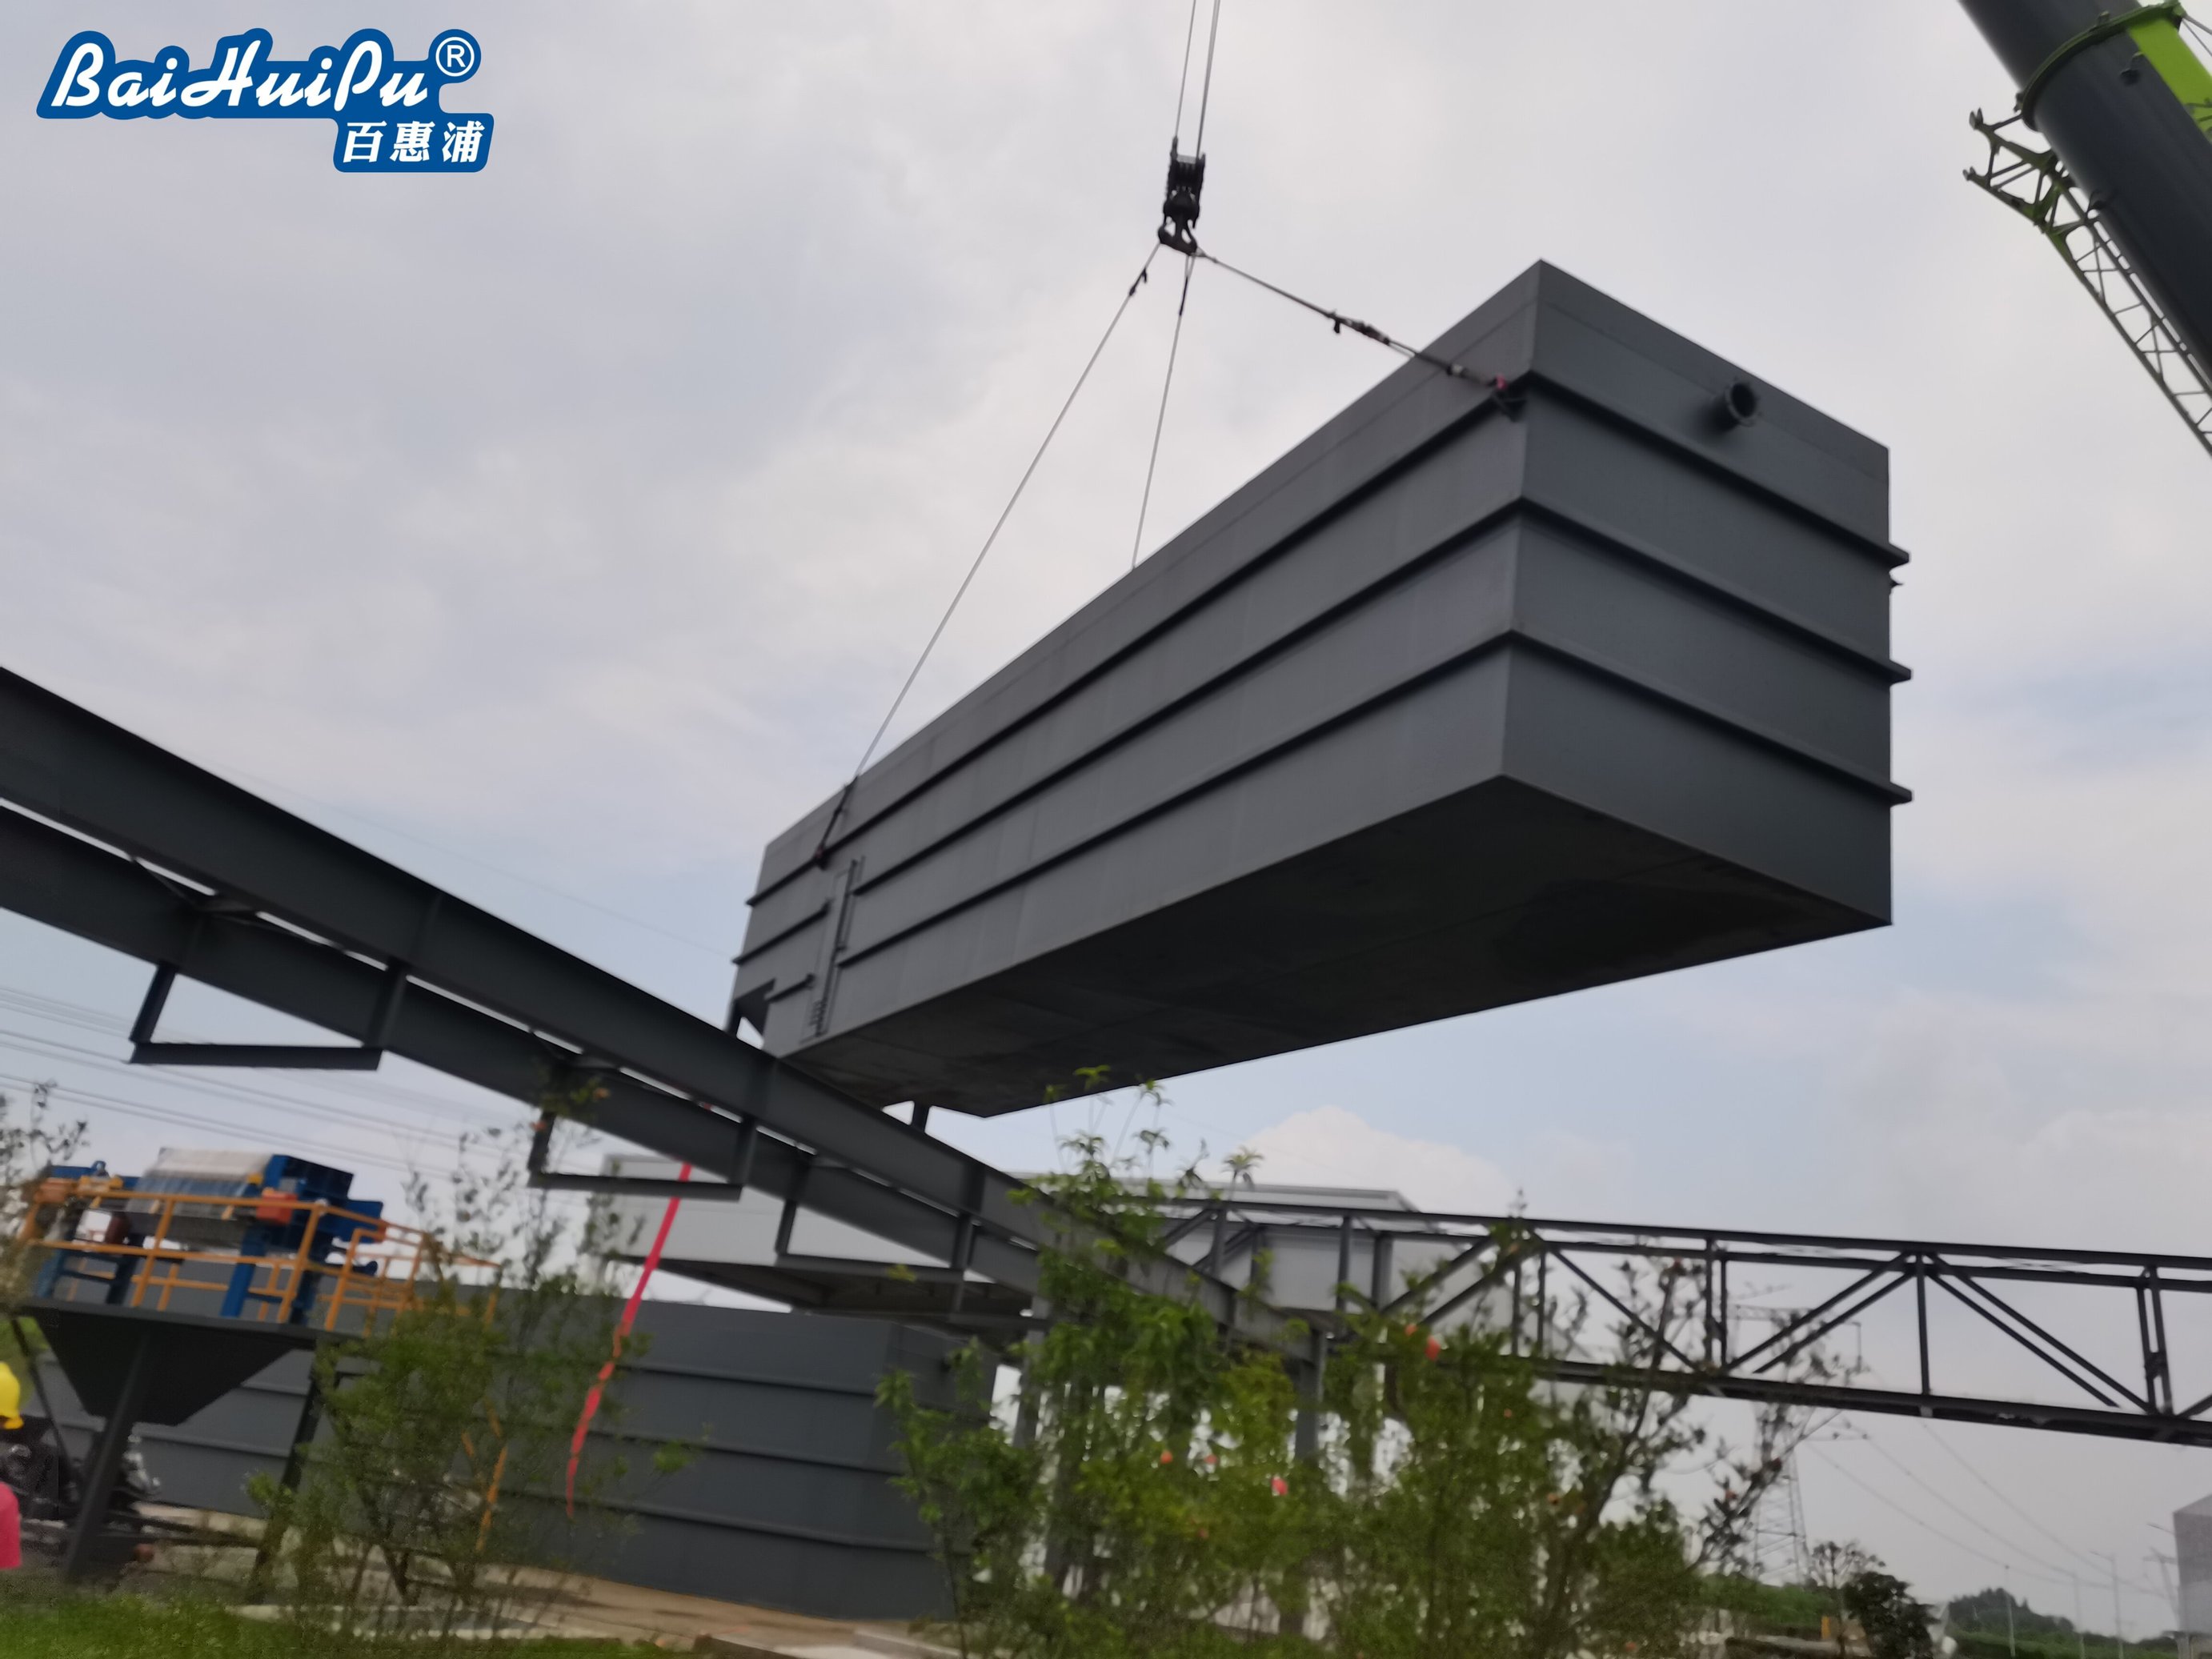
The system effectively removes:
The treated wastewater consistently meets industry discharge requirements.
The treatment process delivers reliable long-term performance with minimal fluctuation in water quality, making it suitable for either direct discharge or industrial water reuse.
The system can be configured to recover valuable metals such as gold (Au) and silver (Ag) from selected wastewater streams, supporting resource recycling while reducing production costs.
Through optimized process design and intelligent equipment control, the system minimizes power consumption while maintaining excellent treatment performance, resulting in lower operating costs.
The modular system design requires relatively little installation space, making it suitable for facilities with limited available plant area.
The entire plant is controlled through a PLC-based automatic control system that provides:
The complete treatment process operates within a closed system, minimizing odor emissions and preventing secondary pollution while protecting both the factory environment and surrounding ecosystems.
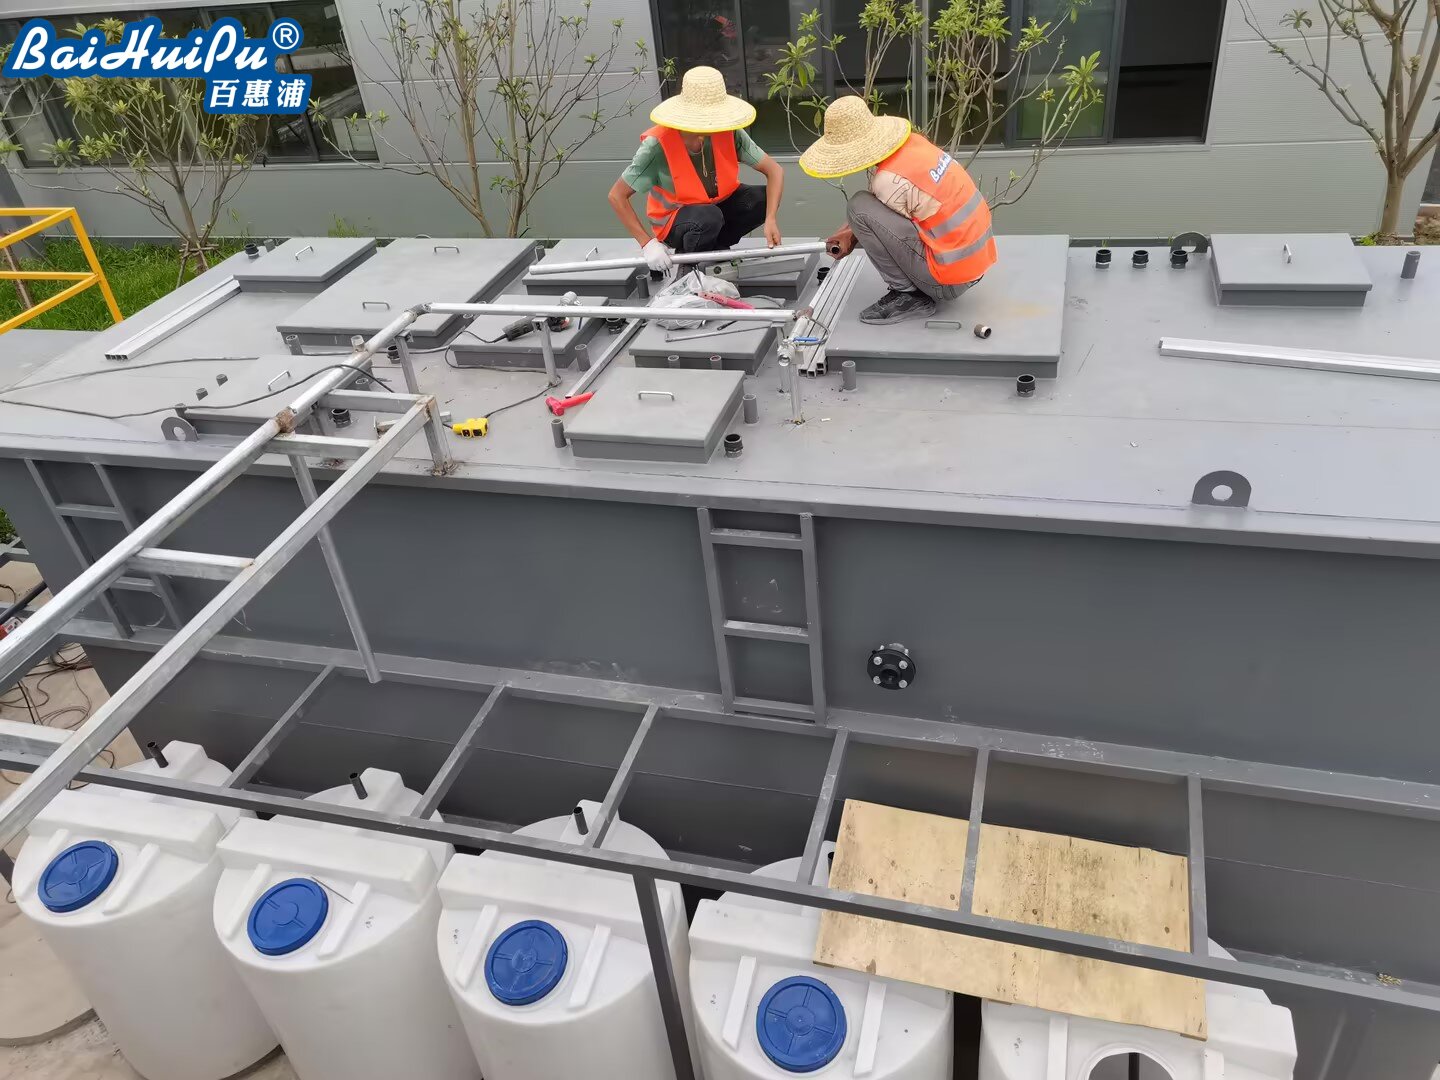
Several technical challenges were encountered during project implementation.
Wastewater quality varied significantly due to continuous battery production, requiring 24-hour online monitoring and dynamic adjustment of chemical dosing and operating parameters.
Solution: Baihuipu implemented intelligent monitoring systems combined with automated process optimization to maintain stable treatment performance despite fluctuating influent conditions.
Certain heavy metal ions existed in highly complexed forms that were difficult to remove using conventional precipitation chemicals.
Solution: The engineering team optimized the precipitation chemistry by selecting specialized heavy-metal treatment reagents and precisely controlling chemical dosing according to wastewater characteristics.
Long-term operation of a large-scale treatment facility required effective control of maintenance costs and consumable replacement.
Solution: Baihuipu established a standardized preventive maintenance program together with optimized operating procedures, significantly reducing lifecycle operating costs while ensuring reliable system performance.
Leveraging many years of experience in battery wastewater treatment, Baihuipu successfully delivered a highly efficient and reliable wastewater treatment system tailored to the customer's manufacturing requirements.
Since commissioning, the project has demonstrated stable long-term operation, consistent compliance with environmental discharge standards, low operating costs, and simplified maintenance.
Through continuous process optimization and a standardized equipment management program, the system provides reliable environmental protection for battery manufacturing while supporting sustainable production, regulatory compliance, and long-term operational efficiency.
Today, the project serves as another successful reference for Baihuipu's expertise in providing turnkey wastewater treatment solutions for the rapidly growing global new energy battery industry.

 EN